Geometry review
Material conductivity, workpiece thickness, start-hole access, profile geometry, corner requirements and datum strategy are reviewed.
EDM Machining
Wire EDM cutting for conductive metals, hardened tooling components and complex through-profiles manufactured to customer drawings.
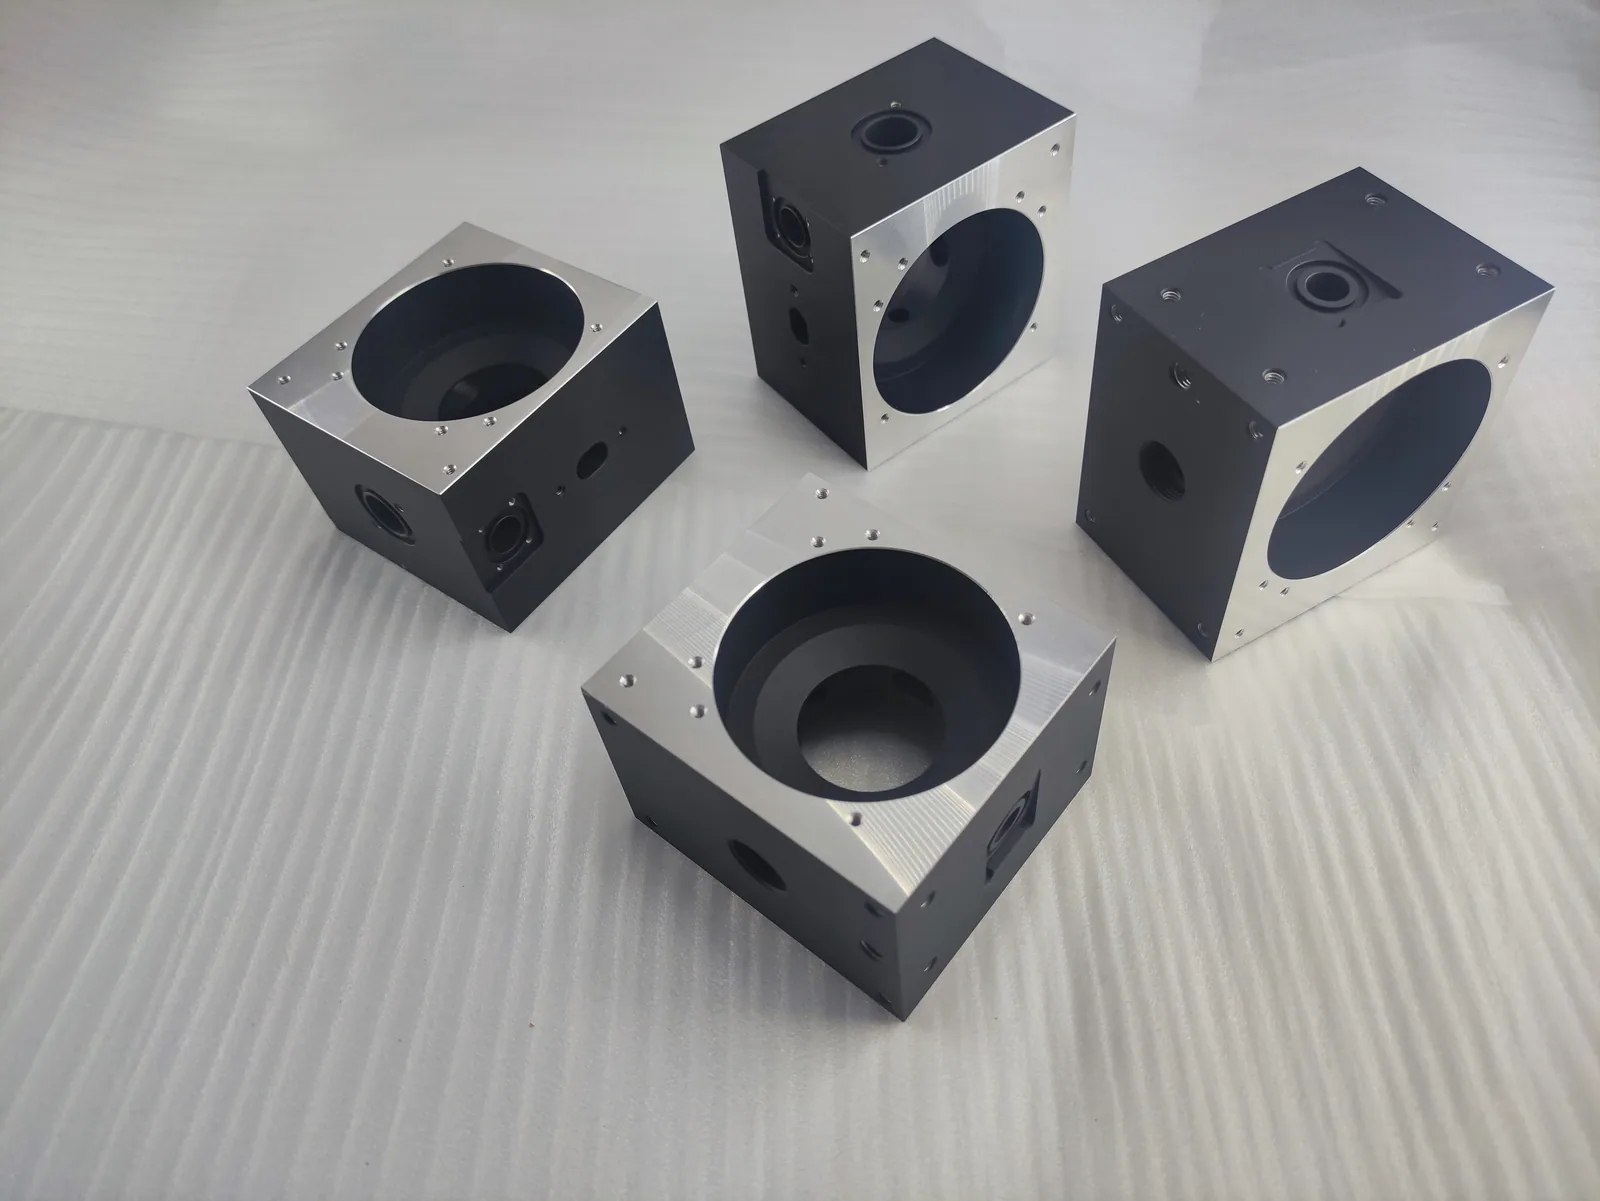
Capability overview
Precision wire EDM support for complex profiles, narrow slots, hardened conductive materials and drawing-led dimensional inspection.
Project workflow
Material conductivity, workpiece thickness, start-hole access, profile geometry, corner requirements and datum strategy are reviewed.
Wire path, workholding, cutting sequence and inspection references are planned around the controlled drawing.
Rough and finishing passes are selected according to geometry, surface requirement and project-specific dimensional needs.
Critical profiles, slots, tapers and feature relationships are checked using the agreed inspection method and reporting scope.
Product examples
Images illustrate the component families and application context relevant to this capability.
Materials
Applications
Surface finishing
Anodizing, coating, plating, passivation and mechanical finishes can affect dimensions, masking, color and inspection. Compare the options before submitting your RFQ.
Compare surface finishesMolding & tooling
Plastic injection molding, metal injection molding, export molds, metal stamping and die casting have different material, geometry, volume and ownership requirements.
Compare molding and tooling optionsService and RFQ scope
These terms describe common project types and RFQ requirements. Final capability, material availability and documentation are confirmed against your drawing.
Wire EDM can support conductive materials, intricate profiles and tooling features where low cutting force is useful.
Frequently asked questions
Project-specific capability depends on the drawing, material, quantity and inspection requirements.
Read the RFQ checklistProvide the 3D model and controlled drawing with material, heat-treatment condition, thickness, quantity, critical profiles, surface requirements and inspection needs.
Wire EDM can process electrically conductive hardened steels without relying on conventional cutting force. Final capability still depends on material, thickness and geometry.
A closed internal cut normally requires a suitable start-hole or another defined wire-entry approach. Identify existing holes and surfaces that must remain untouched.
Tapered and intricate through-profiles can be reviewed, subject to workpiece thickness, machine access, angle, corner geometry and the required inspection method.
Send the key project details and our manufacturing team will respond with a focused next step.