For engineers and sourcing teams, the right CNC route depends on tool access, datum relationships, setup count, inspection and volume—not on choosing the machine with the most axes.
Key takeaways
Choose 3-axis machining when critical features are accessible with simple, repeatable workholding.
Consider 3+2 or simultaneous 5-axis machining when compound angles, multi-face features or cross-face datum relationships drive the process.
Compare total part cost—including fixtures, setups, deburring and inspection—not machine hourly rate alone.
01
Understand 3-axis, 3+2 and simultaneous 5-axis machining
In 3-axis milling, the cutter moves along X, Y and Z while the workpiece remains fixed during each cutting operation. Features on another face normally require the part to be repositioned in a new setup.
Five-axis equipment adds two rotary axes. In 3+2 indexed machining, the machine positions the part at an angle and then cuts with the rotary axes locked. In simultaneous 5-axis machining, linear and rotary axes move together to follow complex surfaces or maintain tool orientation. These are different process strategies and should not be treated as interchangeable labels.
- 3-axis: linear motion with separate setups for additional orientations
- 3+2 machining: indexed access to angled or multi-face features
- Simultaneous 5-axis: coordinated motion for contoured surfaces and changing tool angles
- The drawing and geometry determine which strategy is justified
02
Choose 3-axis machining for accessible, fixture-friendly parts
Three-axis machining is usually practical when the important features are visible from one main direction or can be reached through a small number of simple, stable setups. Plates, brackets, open pockets and straightforward housings often fit this profile.
Repeatable fixtures can also make 3-axis machining effective for features on several sides, especially at production quantities. Using five-axis equipment for geometry that gains no meaningful access or datum benefit can add programming effort without reducing total cost.
- Planar faces, open pockets and vertical holes
- Critical features concentrated on one or two orientations
- Adequate clamping surfaces for repeatable secondary setups
- Volumes that justify simple dedicated fixtures
03
Choose 5-axis access when geometry or relationships demand it
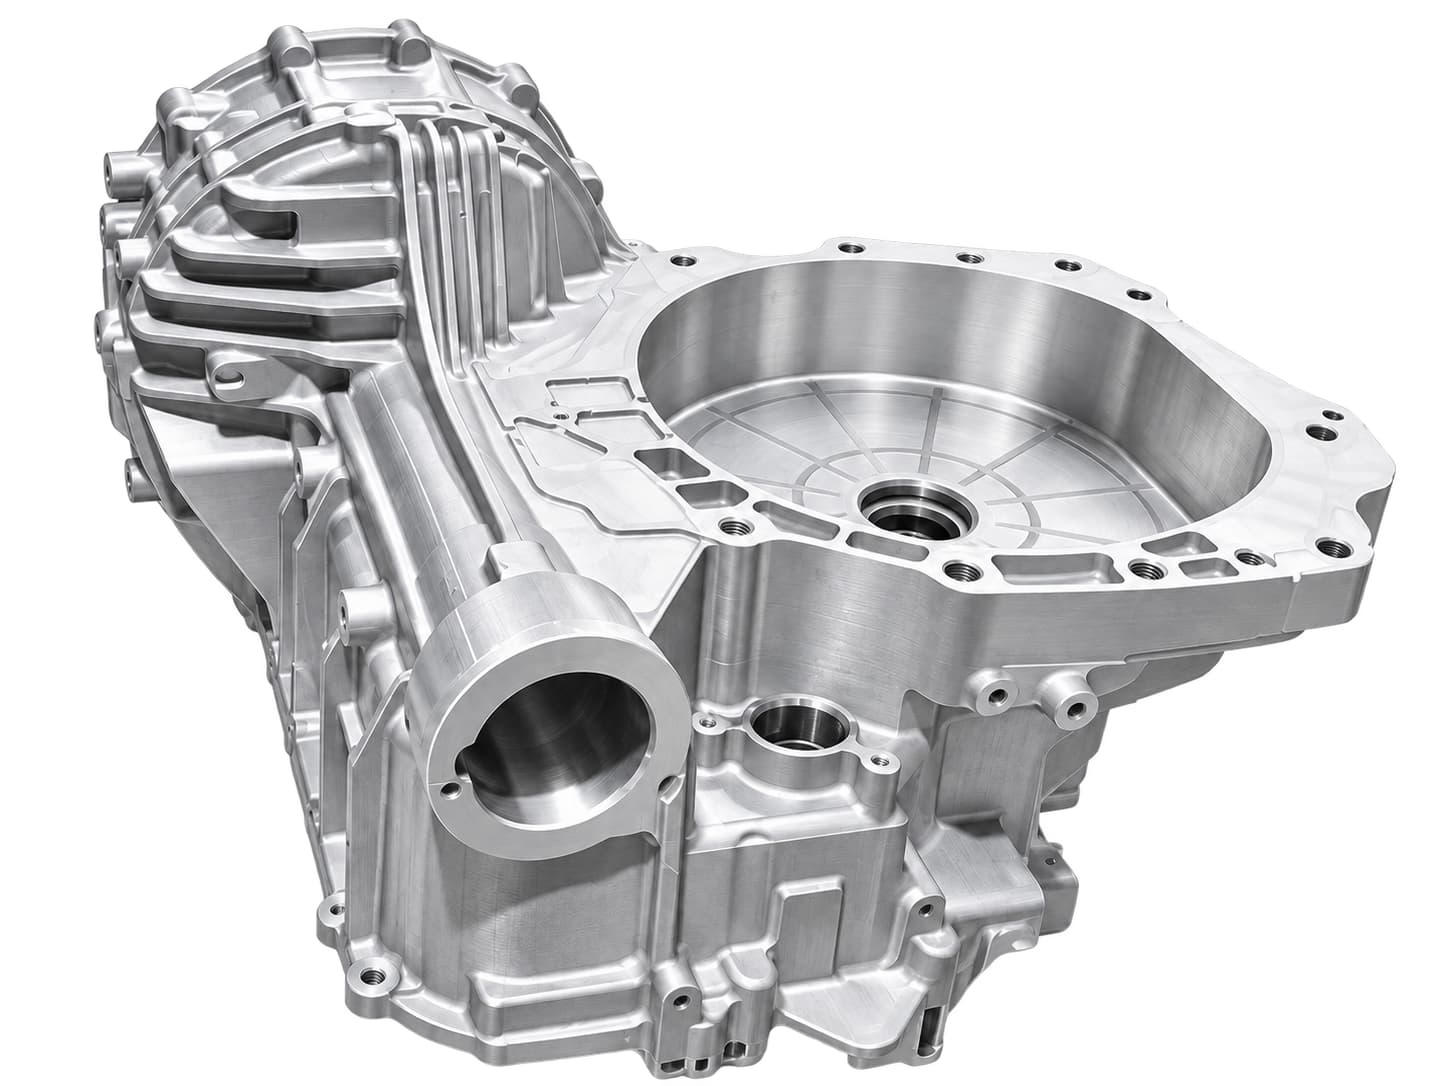
Five-axis access becomes valuable when the cutter must reach compound-angle holes, multiple faces, undercut-adjacent areas or contoured surfaces. It can also reduce the number of times a part is unclamped and realigned.
The strongest reason is often not visual complexity but a functional relationship. If bores, sealing faces and mounting features on different sides reference common datums, machining more of them in one controlled setup may reduce alignment risk. A shorter tool orientation can also improve rigidity and access, although results still depend on workholding, programming and the feature itself.
- Compound-angle holes, ports and sealing features
- Features distributed around several faces
- Closely related cross-face bores and mounting interfaces
- Sculpted or continuously changing surfaces
- Areas where long tool reach would reduce rigidity
04
Compare setups, datums and inspection before selecting the route
Every new setup creates another workholding and alignment condition. That does not make multiple setups unacceptable, but it means the process must control how datums are transferred from one operation to the next. Review which features are created together and which tolerance relationships cross setup boundaries.
Inspection must be planned at the same time. A five-axis machine does not remove the need for a functional datum scheme, accessible measurement features or an agreed reporting scope. Flexible or thin-wall parts may also need a defined inspection condition so manufacturing and quality teams evaluate the same state.
- Count required orientations and reclamping steps
- Mark critical relationships that span different faces
- Confirm stable clamping and datum surfaces
- Define how position, profile and runout will be measured
- State whether inspection is before or after finishing
05
Evaluate total part cost rather than machine rate
The hourly rate of five-axis equipment is only one input. Programming, fixtures, setup labor, cycle time, tool reach, deburring, inspection and scrap risk all affect the quoted part cost.
A 3-axis route with several predictable operations may remain the lowest-risk choice. A 3+2 or simultaneous 5-axis route may be more economical when it replaces complex fixtures, reduces manual alignment or improves access to several critical features. Prototype quantity and repeat volume can change the answer because one-time setup effort is distributed differently.
- Programming and prove-out time
- Fixture count and complexity
- Recurring setup and handling time
- Deburring and inspection effort
- Prototype quantity, batch size and annual demand
06
Use this decision checklist before requesting a quote
Start with the part, not a preferred machine name. Send the current 3D model and controlled 2D drawing, then identify the features and relationships that control fit, sealing, motion or assembly. This gives the supplier enough context to compare 3-axis, indexed and simultaneous 5-axis routes.
MIM Machining reviews drawing-led CNC projects against geometry, material, quantities, finishing and inspection needs. Upload the current files and mark any surfaces that cannot be clamped, touched or cosmetically marked so the process recommendation is based on the complete requirement.
- Current CAD model and drawing revision
- Functional datums and critical cross-face relationships
- Material grade, heat treatment and surface finish
- Prototype and production quantity breaks
- Inspection records or first-article requirements
- Target delivery and packaging expectations
Frequently asked questions
Questions engineers and buyers ask before quotation.
Is 5-axis CNC machining always more accurate than 3-axis machining?+
No. Accuracy depends on the complete process, including machine condition, workholding, tooling, thermal control, programming and inspection. Five-axis machining can reduce datum transfers for multi-face features, but a stable 3-axis process can be the better choice for accessible geometry.
What is the difference between 3+2 and simultaneous 5-axis machining?+
In 3+2 machining, the rotary axes position the part and remain fixed during cutting. In simultaneous 5-axis machining, rotary and linear axes move together while the tool cuts. Simultaneous motion is mainly justified by complex surfaces or changing tool orientations.
When can 5-axis machining reduce total cost?+
It may reduce total cost when it replaces multiple fixtures, limits manual realignment, improves access with shorter tools or consolidates critical multi-face features. The saving must be compared with added programming, prove-out and machine time.
What files help a supplier choose between 3-axis and 5-axis machining?+
Provide the current 3D CAD model and controlled 2D drawing, plus material, quantity, finish, critical datums, inspection scope and delivery needs. Identify surfaces that cannot be clamped or marked.
Plan the next step
Continue from guide to project review.
Julie Cai
Project contact connecting international customers with MIM Machining's manufacturing and engineering review team.
Contact Julie